Scaligera Guarnizioni S.p.A.
Rubber and plastics
Energy, compressed air, water in closed-loop circuits and nitrogen: zone-by-zone supervision run in-house, with alarms on abnormal consumption.
Connected manufacturers in Rubber and plastics
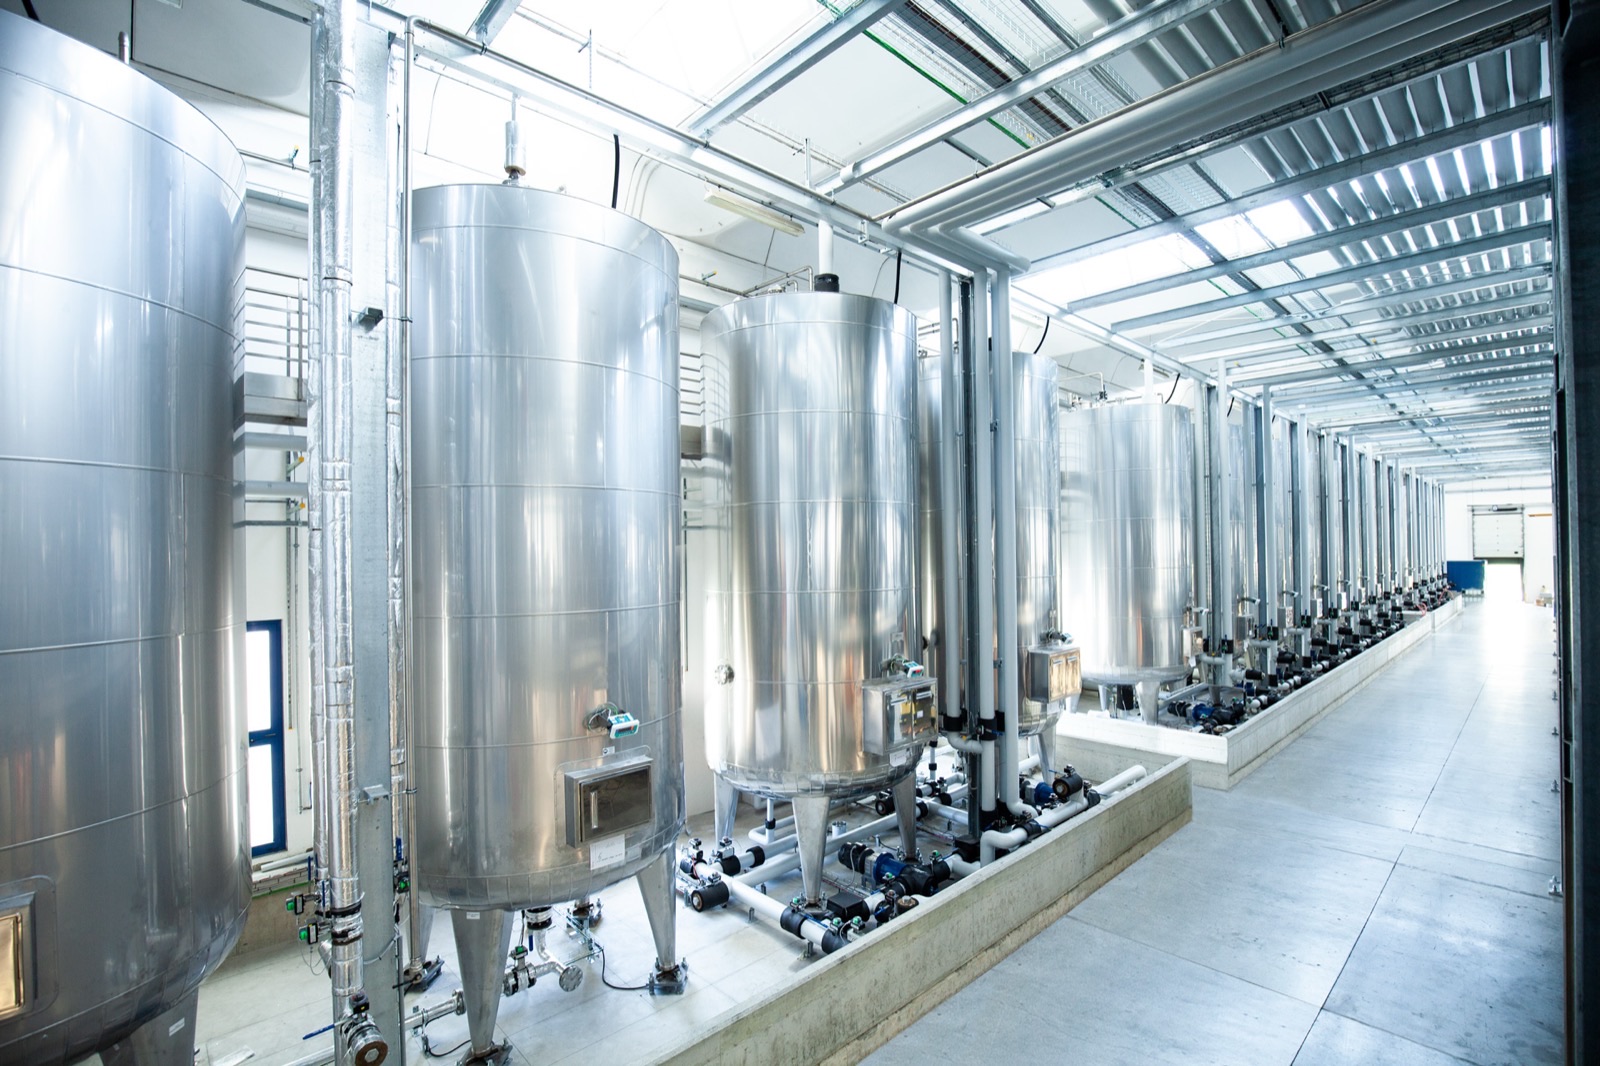
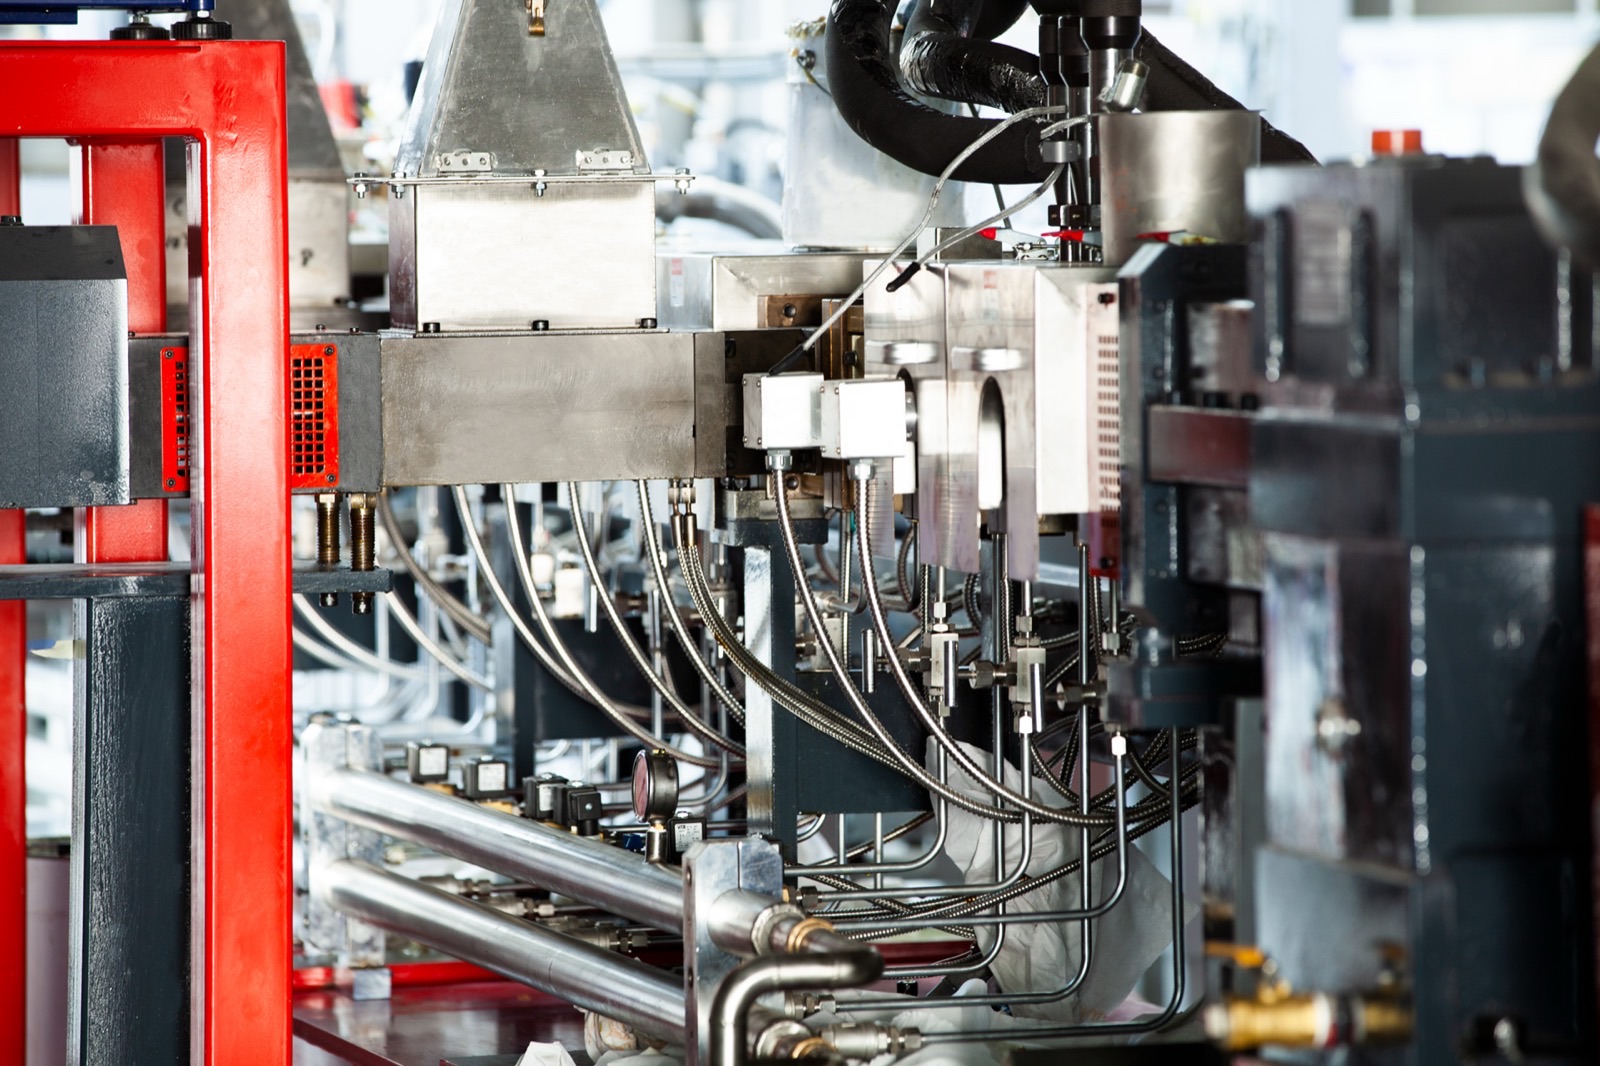
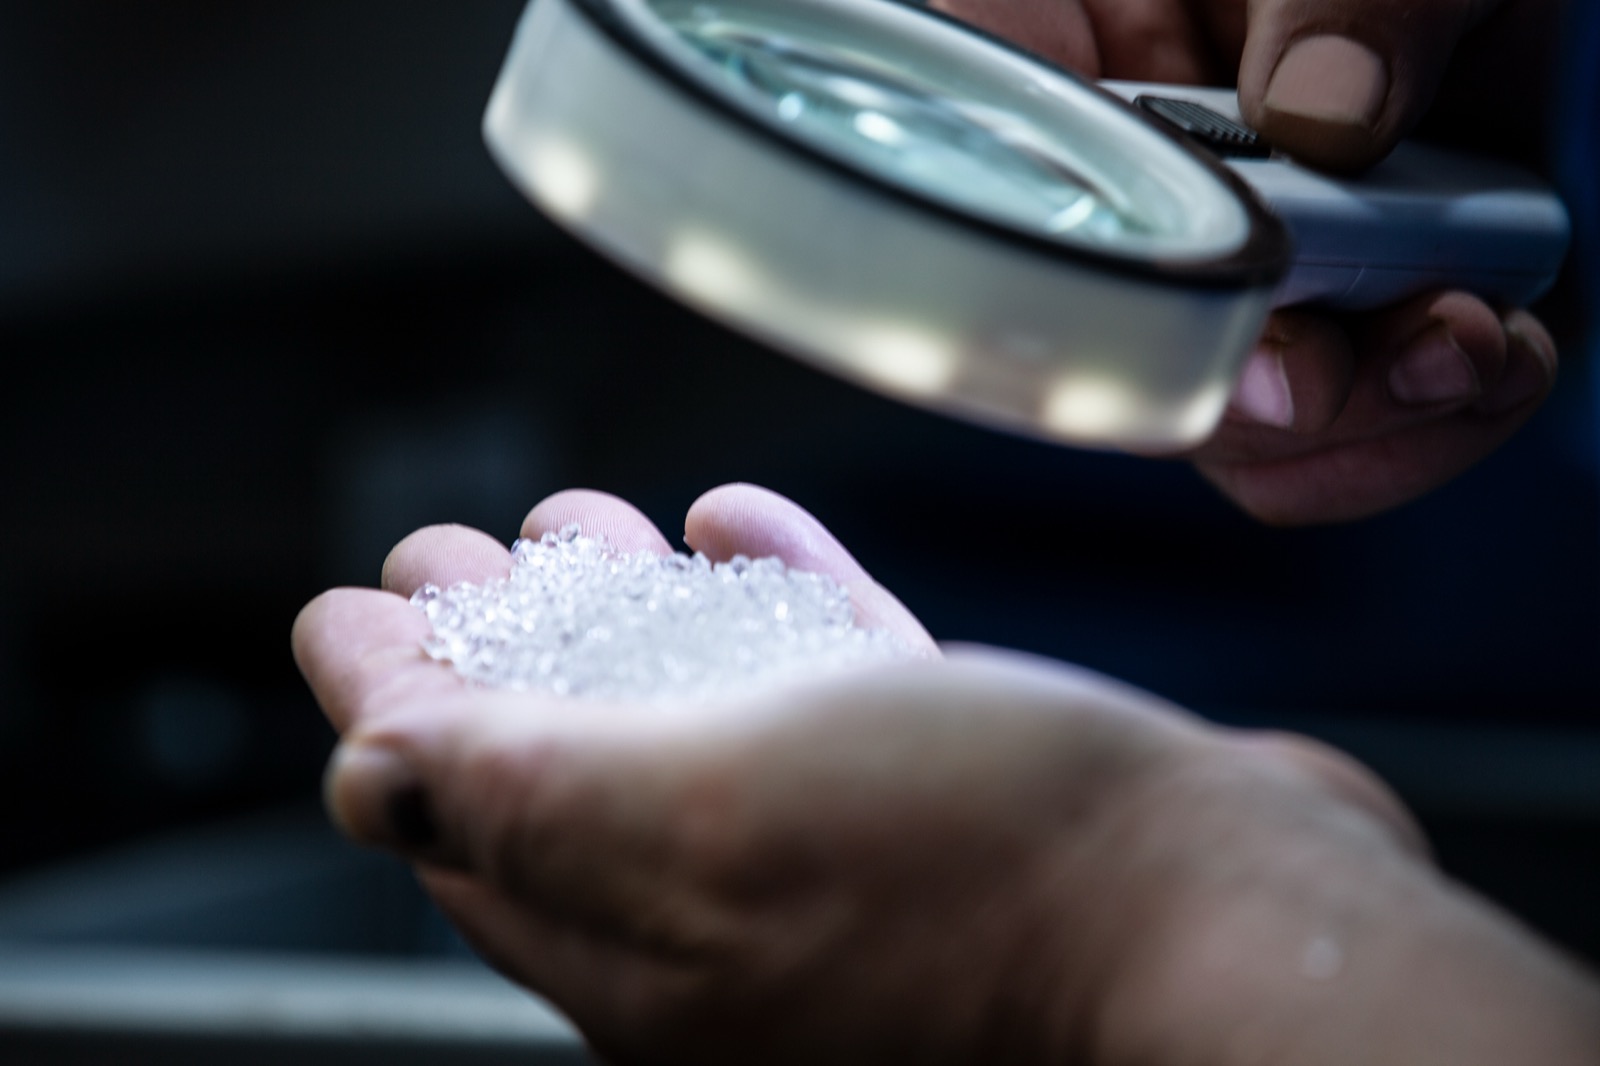
Revo S.p.A., part of the Kairos group and based in Colognola ai Colli (Verona), specialises in producing innovative thermoplastic polyurethanes, with a strong focus on increasingly sustainable solutions. It holds ISO 9001 certification and, with the 2024 renewal of its GRS (Global Recycled Standard) certification, confirms its commitment to sustainability and the circular economy in polymer materials.
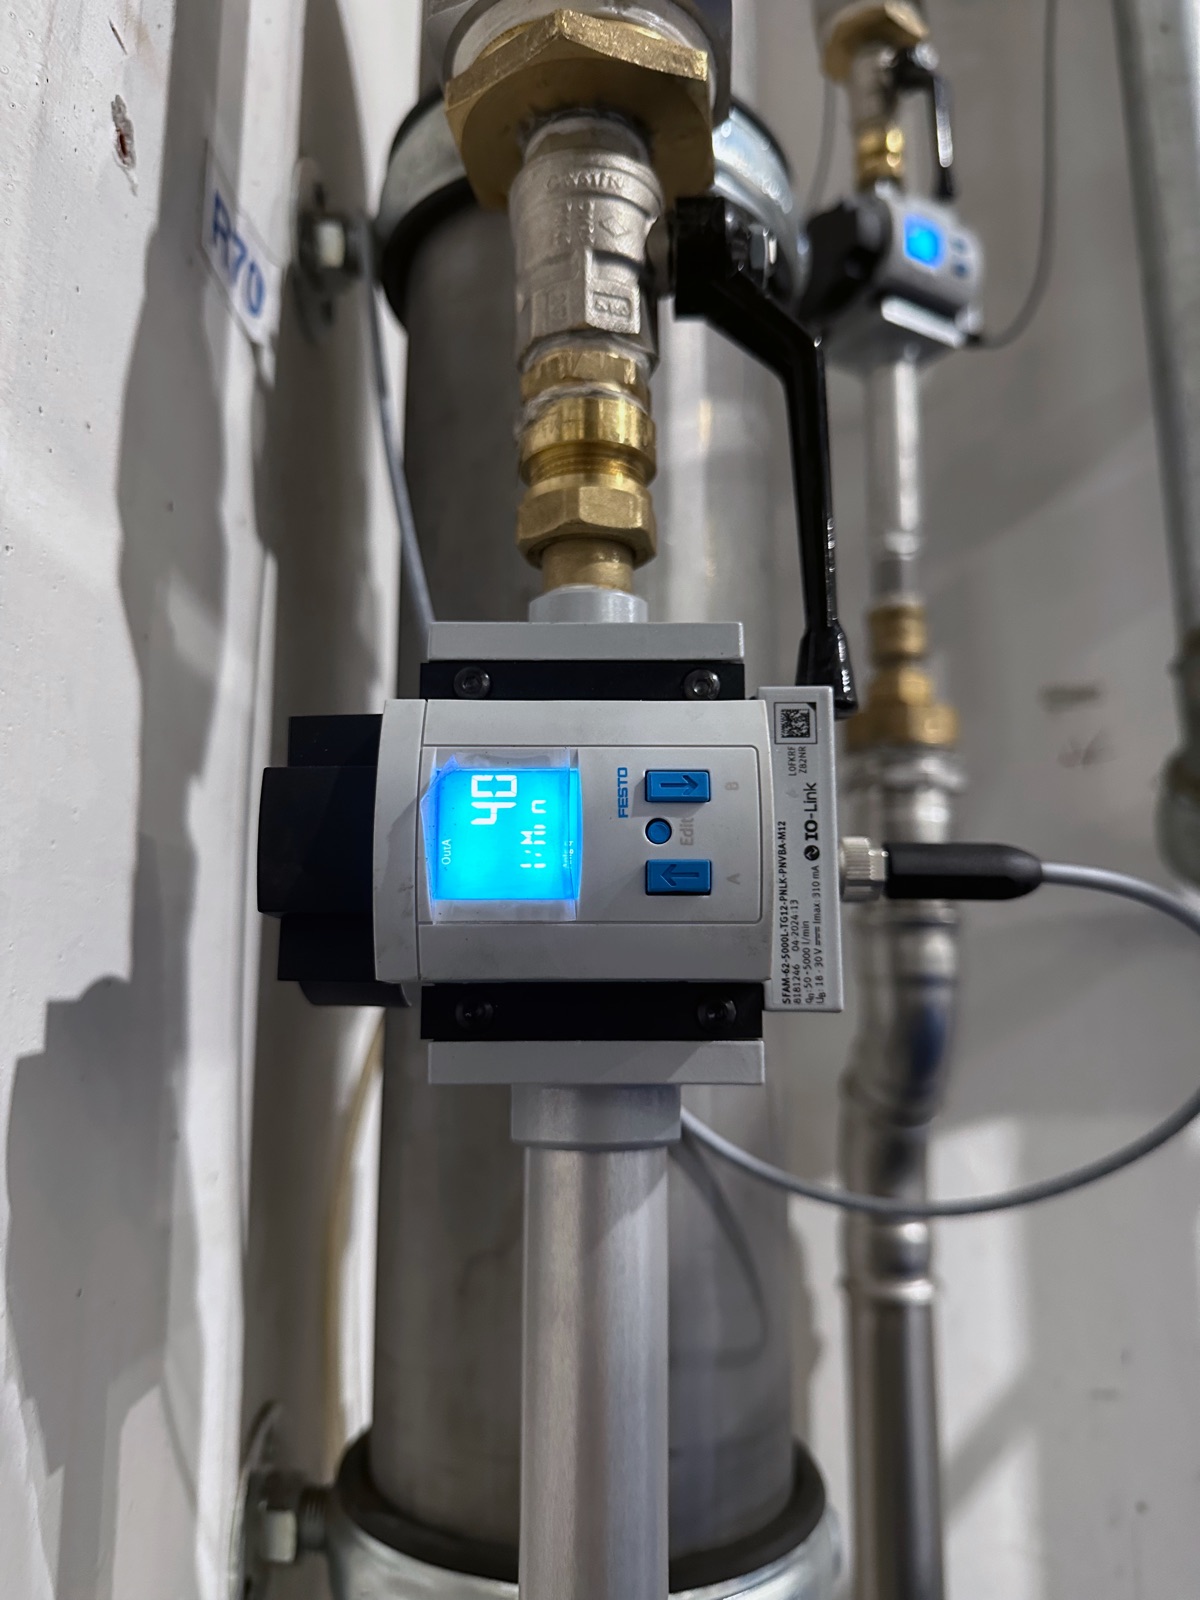
Already running a digital system to monitor the electricity consumed by its production plant, Revo needed to extend monitoring to other metrics, so it could analyse abnormal energy use in context and anticipate potential faults and stoppages. Specifically, it wanted to analyse energy consumption and the compressed air, water and nitrogen used in its production processes.
Maxfone took a step-by-step approach, integrating the energy meters already installed and using IDA to progressively extend energy supervision to every area of the plant.
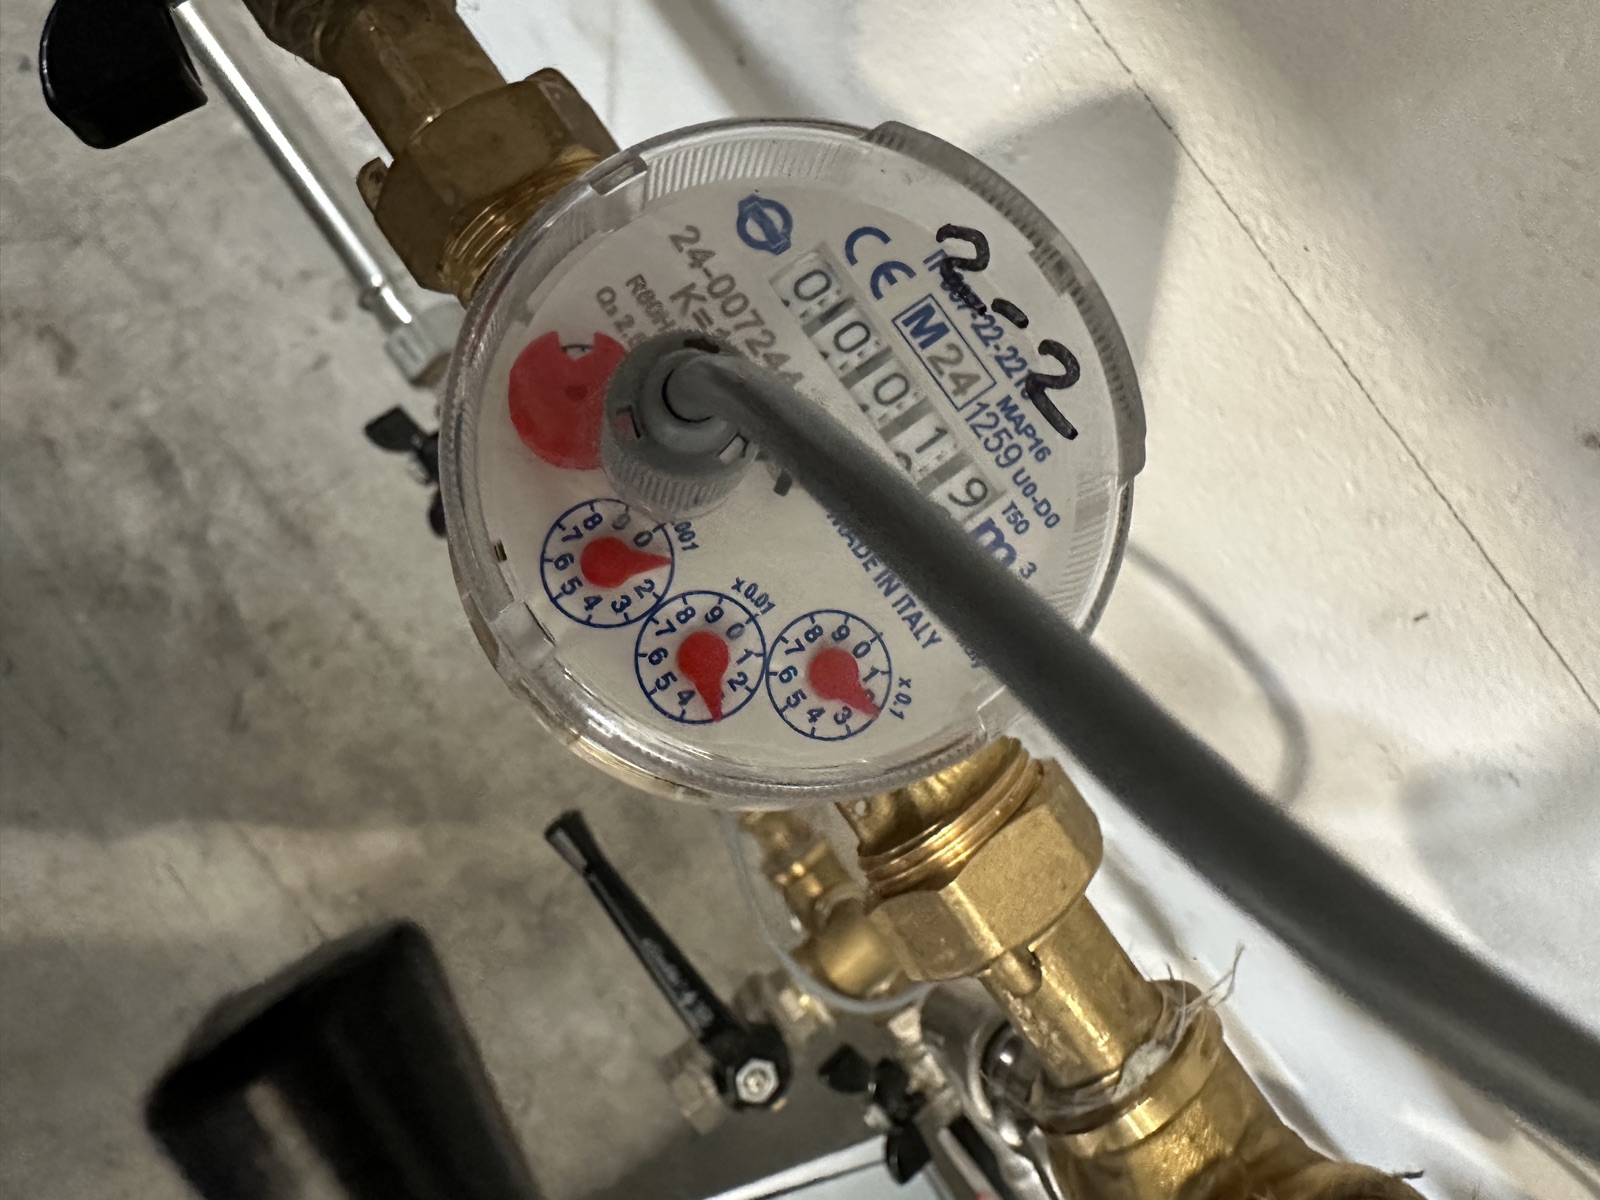
After energy monitoring, Revo asked for a function covering water consumption in closed-loop systems, enabling real-time control of the flow across the plant's three circuits. An alarm system flags abnormal water consumption, so the company can prevent faults and anomalies in production. Supervision was then extended to nitrogen production. With IDA, Revo manages utility consumption by area quickly and intuitively, without needing specialist technical support.
The efficiency, adaptability and speed with which IDA integrates data flows from different sources give Revo the ability to monitor production parameters and safeguard the stability of its core business. That renews its attention to environmental sustainability while keeping the economic focus sharp, cutting the costs of unnecessary energy consumption.
The rollout will continue, moving from a partial view to a complete view of consumption across the whole company. Revo will be able to compare data from its various plants and see whether any machine needs more technical support, setting functional benchmarks that identify anomalies and drift and trigger predictive maintenance protocols. On the sustainability side, work continues on calculating CO₂ equivalent per kilogram of product for each individual batch, to detail the production lines and make Life Cycle Assessments better grounded and more precise.
"Working with Maxfone allows us not only to optimise and monitor all our production processes in real time, reducing and preventing plant downtime, but also to design new, innovative solutions together with expert engineers, tailored to help us grow ever more sustainably."
IDA is already at work in other plants in the Rubber and plastics sector. Read their case studies.
See all connected machinesScaligera Guarnizioni S.p.A.
Rubber and plastics
Zeno S.r.l.
Rubber and plastics
A demo on your sector: it takes us very little to show the impact on your production process.
Request a demo